Shakeout Deck Attrition Mill
Shakeout and attrition systems that increase foundry throughput while cutting labor, scrap, and maintenance costs.
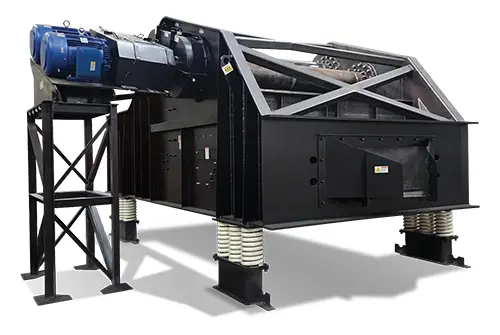
Shakeouts for No Bake Sand, Flasked and Flaskless Applications
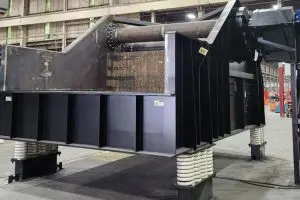
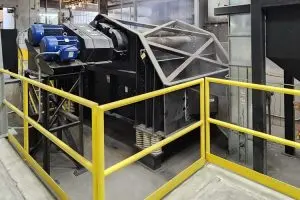
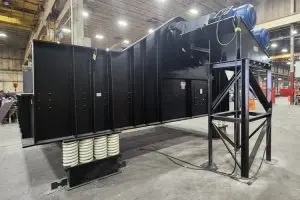
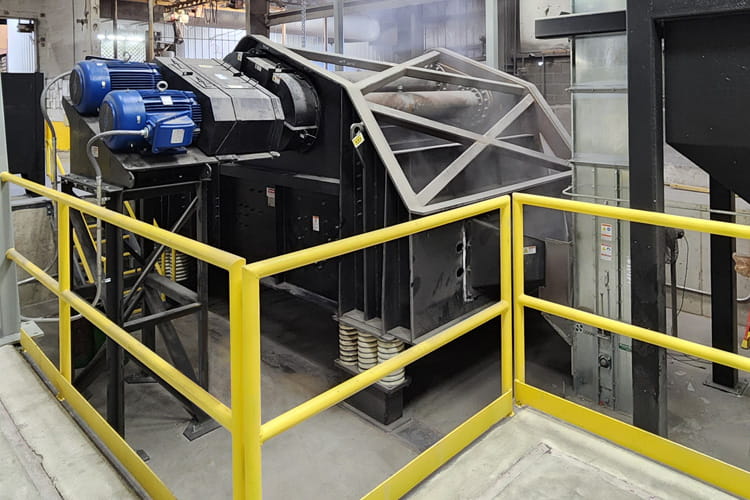
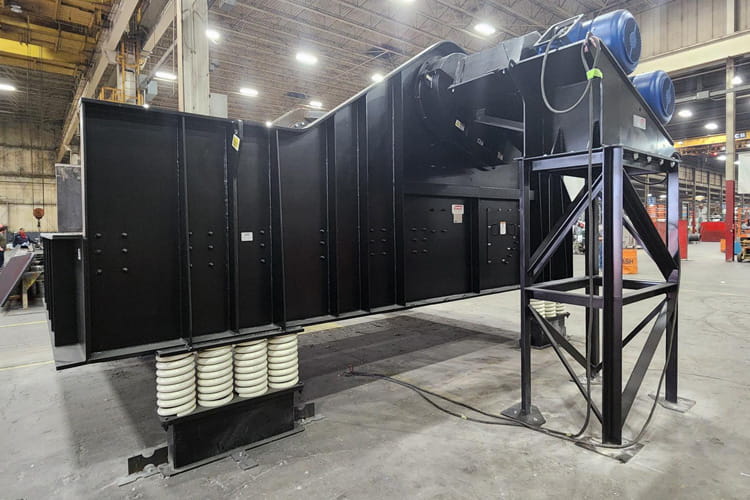
Carrier Vibrating Equipment Shakeout Deck / Attrition Mill Combination Units shake out castings and reduce no-bake sand back to grain size. A vibratory motion separates sand from castings, then processes the sand through a series of three perforated decks and screens, reducing lumps to grain size. This reduces shakeout time and labor for foundry operations running continuous casting cycles. Designs are available for no-bake sand in both flasked and flaskless configurations.
Features & Benefits
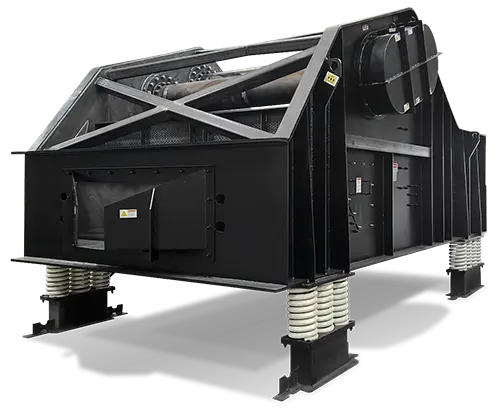
Equipment Options & Accessories
Carrier shakeouts are available in a variety of design configurations depending on the foundry application.
Space-saving design for facilities with space constraints.
Ability to handle up to 100‑ton loads: useful for heavy castings or large mold flasks.
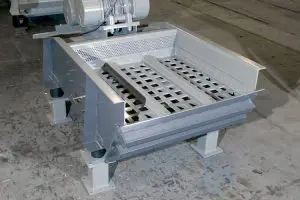
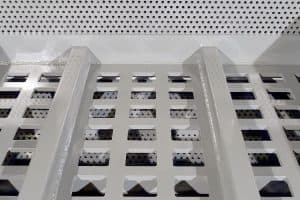
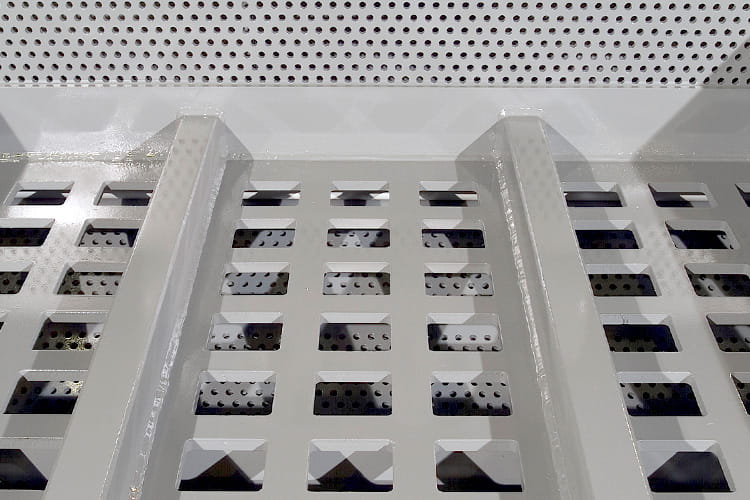
Decks for large flask sizes or heavy molds, “V” shaped decks for engine blocks, grizzly designs for maximum large-lump scalping and separation, and back-drafted slots to prevent damage to fragile castings.
Heavy-duty wear liners and specialized sand pans are available, including moisture-resistant options for handling wet sand.
Available in multiple designs, including energy-efficient natural frequency, sub-resonant two-mass drives, and brute force direct drives.
Available in low or high vibration designs to process the widest range of materials.
Simple starter panels or customized PLC-based controllers complete with remote startup and engineering services. Controls are tailored to specific casting requirements, utilizing advanced, pre-programmed sequences to control vibration and retention time.
Applications
Uses controlled vibratory energy to separate molding sand from castings after pouring. Engineered stroke and frequency promote efficient sand removal while minimizing casting damage and unnecessary handling.
Breaks no-bake molds down into small lumps to prepare for downstream attrition to be followed by mechanical and/or thermal reclamation.
Separate solid, chemically bonded sand molds from metal castings while breaking the molds down to smaller lumps.
Accommodates common molding aggregates like silica sand as well as specialty sands used for complex metal castings.
No-bake and green sand shakeouts safely separate hardened sand from metal castings and empty the sand from the foundry flask. The heavy-duty vibratory action knocks the sand out without degrading or damaging the fragile metal casting.
Efficiently separate rigid sand molds from metal castings and break down sand lumps without damaging the finished part. For flaskless molding, this process is critical for safely stripping away chemically bonded sand and preparing it for downstream reclamation.
Breaks down chemically bonded molds and separates sand from castings using engineered vibratory energy. Effective lump reduction prepares bonded sand for subsequent attrition, reclamation, and reuse. Primarily designed for No-Bake systems (e.g., Phenolic Urethane No-Bake (PUNB), furan, or ester-cured).
SDAM Shakeouts FAQs
There is a series of three decks/screens sand must pass through before being discharged. Primary deck is where the castings are shaken out, picked off, and then the remaining mold sand is reduced to ~4″ maximum lumps. The secondary screen is below/ahead and forms an attrition chamber to break sand back down to grain size with holes of ~1/2″ diameter. Finally, a mesh screen at the discharge removes any oversize particles or agglomerated grains prior to being discharged for downstream processing.
Any type of casting in a no bake mold can be processed on a SDAM, whether steel, iron, aluminum, or other non-ferrous metal.
Yes. Large chills can be picked manually off the primary deck. Smaller chills that pass through the primary deck will be retained ahead of the secondary screen. There are easily removable access doors on both sides of the unit to allow small chills to be emptied from the SDAM.
Yes – Hot molds are no problem for the SDAM as it is all steel and does not include any rubber components that could melt. Care should be taken to make sure that any downstream equipment such as bucket elevators or belt conveyors are rated for the sand temperature processed.
Periodic greasing/oiling of the motors/drives and regular spring inspection/replacement. Decks and screens should also be inspected/replaced on a regular basis as worn out by sand abrasion. We offer decks in mild steel, AR400 abrasion resistant steel, manganese, or other specialty metals as desired.