Elevadores y elevadores en espiral
Spiral elevators provide extremely flexible processing of a range of materials. They offer a compact, energy-efficient solution for vertically conveying, drying, cooling, or processing bulk materials and often eliminate the need for a dryer or cooler. Carrier spiral elevators are recognized throughout the industry for reliable performance and easy maintenance. They minimize material degradation through gentle, harmonic vibration, and deliver low-maintenance and continuous operation, making them ideal for delicate or demanding applications in the food, dairy, rubber, and chemical industries.
Spiral Elevator Equipment
Customized To Your Application
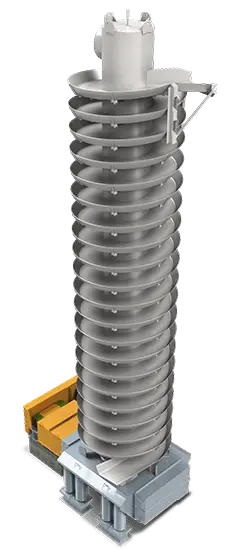
Simultaneous Processing
While elevating, Carrier’s Spiral Elevator unit can heat, cool, dry, or activate material through specialized, optional jacketed flights or air handling. Its smooth, resonant vibration prevents damage to delicate products, unlike traditional bucket elevators. With few moving parts, these systems offer high reliability and minimal downtime, avoiding the wear issues of chain-driven systems.
Elevadores espirales vibratorios
Elevate bulk materials efficiently within a compact footprint while supporting gentle handling and reliable performance. Spiral elevators provide flexible vertical conveying and can be engineered to cool, dry, heat, or condition materials during transport, helping streamline processing and reduce equipment requirements.
Spirals for Foundry
Engineered for demanding foundry environments, Carrier spiral elevators provide reliable vertical conveying for hot castings, sand, and other challenging materials while supporting cooling and process efficiency. Gentle controlled material movement minimizes damage to castings and supports consistent downstream processing. Built for durability and continuous operation.
The Basic Theory of Spiral Elevators
Los elevadores espirales vibratorios utilizan los mismos principios de vibración que los transportadores vibratorios para mover materiales. Sin embargo, el elevador en espiral tiene un canal de forma helicoidal en lugar de un canal largo y recto. El material se introduce a través de una boca de alimentación situada en la parte inferior de la unidad y asciende a medida que se desplaza en círculos alrededor de un tubo central. El material se descarga del elevador en espiral a una altura de hasta 60 pies por encima del punto de alimentación.