Vibrationsförderer
When consistency, efficiency, and reliability matter, does your production line deliver?
Vibrationsförderer
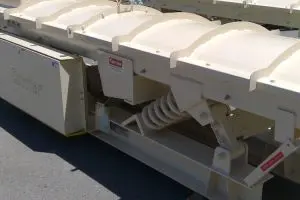
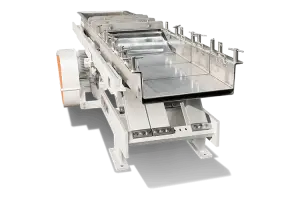
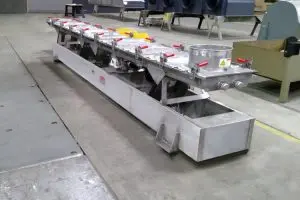
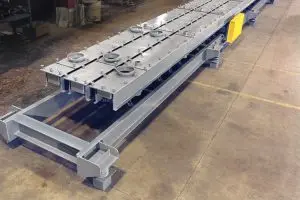
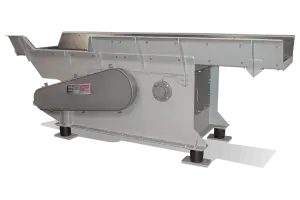
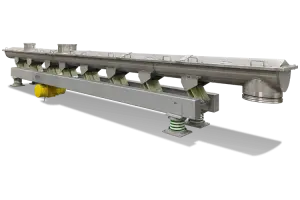
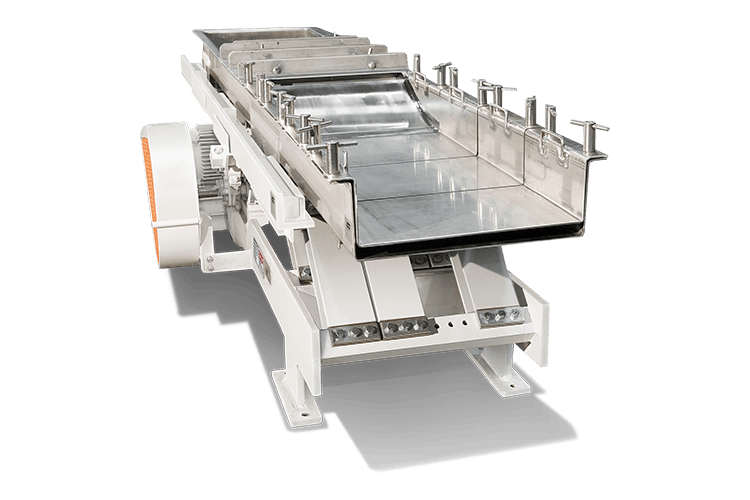
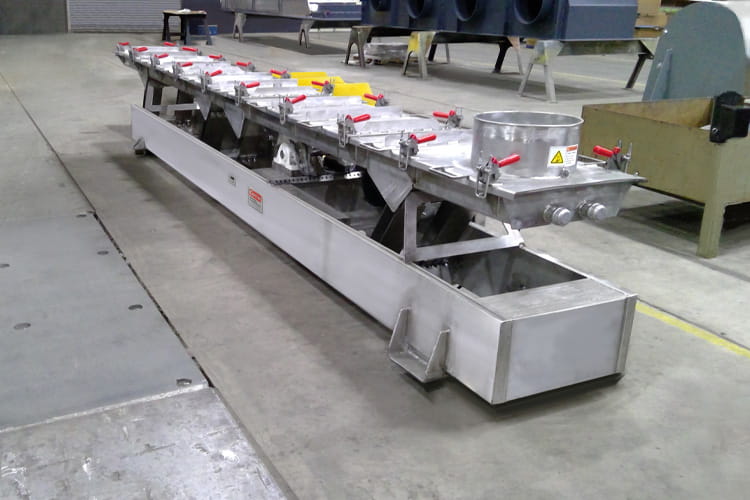
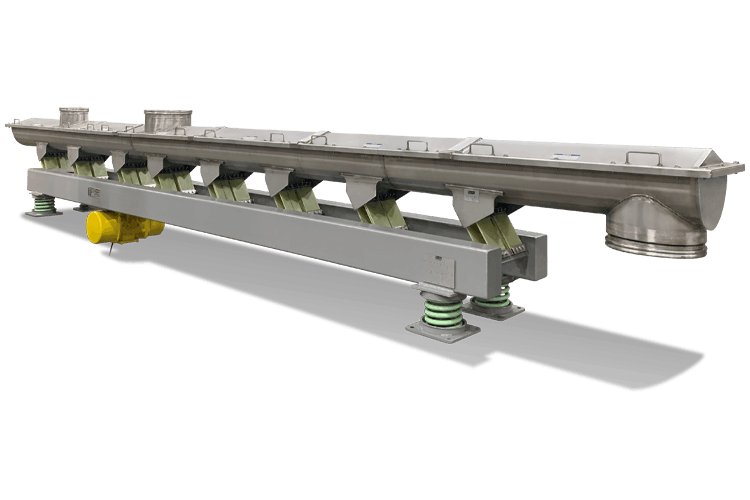
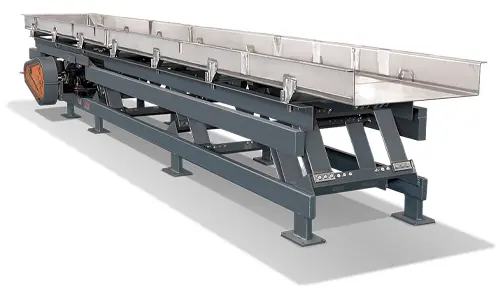
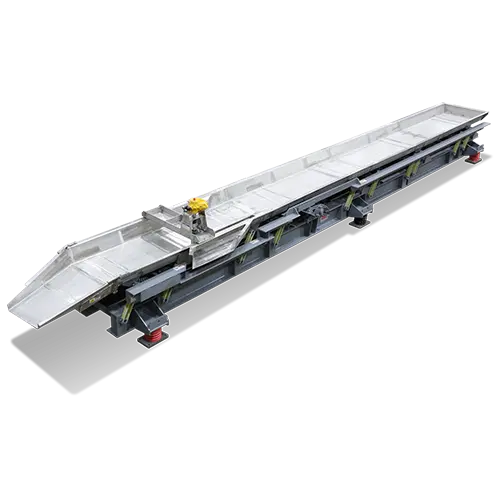
Carrier Vibrating Conveyors provide an efficient and economical method of moving powders and bulk solids. Vibrating conveyors offer an efficient and economical way of gently moving bulk solids, and can be custom engineered to handle everything from light and fragile to heavy and abrasive products. Carrier’s vibrating conveyor units can be multifunctional, and are able to convey, dry, cool, scalp, screen, quench, dewater, orient, accumulate, separate, distribute and more.
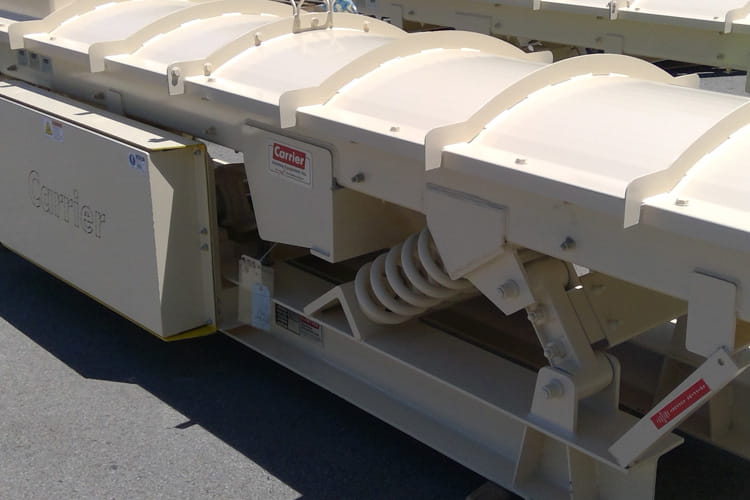
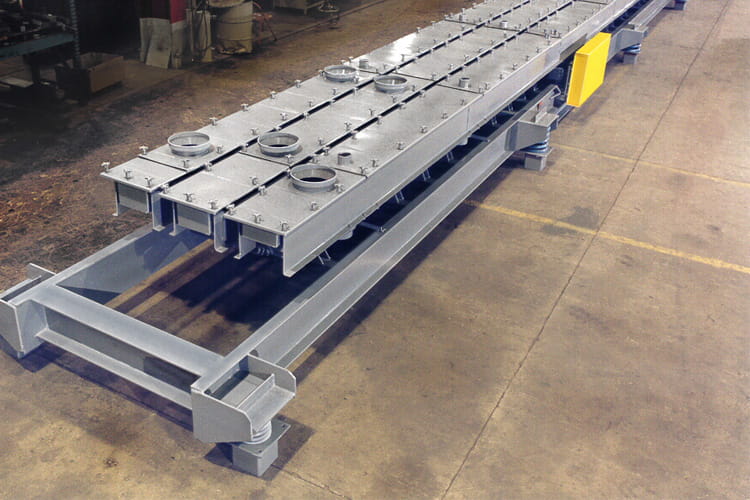
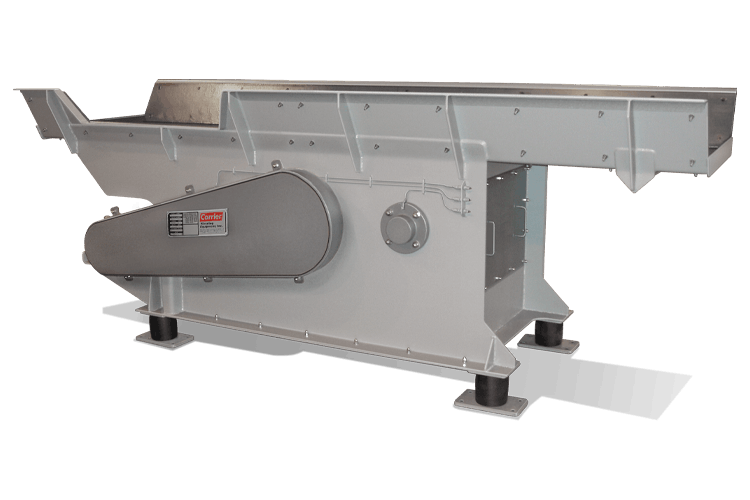
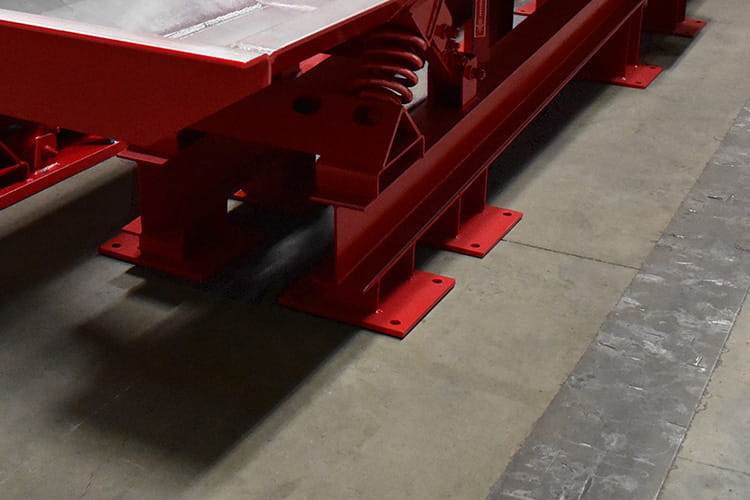
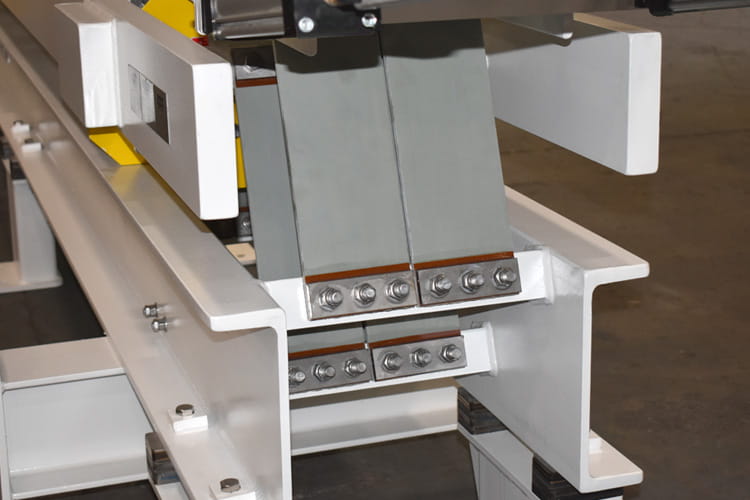
Unsere Schwingförderer zeichnen sich durch eine Eigenfrequenzkonstruktion aus, bei der ein spezieller Antrieb zum Einsatz kommt, der in Resonanz mit dem federunterstützten Gewichtssystem abgestimmt ist, so dass ein Großteil der Antriebsenergie von den Federn gespeichert und wieder abgegeben wird. Einmal in Bewegung, hält die Eigenfrequenz den Förderer in konstanter Bewegung und der gleichmäßige Abstand der Federn sorgt für eine gleichmäßige Verteilung der Antriebskräfte bei Belastung. Diese hocheffiziente und zuverlässige Konstruktion ermöglicht den Betrieb von Förderern mit einer Länge von mehr als 300 Fuß mit einem einzigen Antrieb. Unsere auf Ihre Bedürfnisse zugeschnittenen Förderer sind nachweislich zuverlässig und einfach zu warten.
Features & Benefits
Equipment Options & Accessories
Convey in two directions if the process has more than one path.
Perforated plates or screens can be included to scalp overs, remove fines or dewater products.
Custom dust-tight construction eliminates product degradation and improves operational safety.
USDA/3A certified conveyors for sanitary processing.
Clean-in-place (CIP) systems with spray nozzles can be incorporated into conveyors.
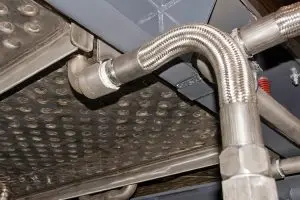
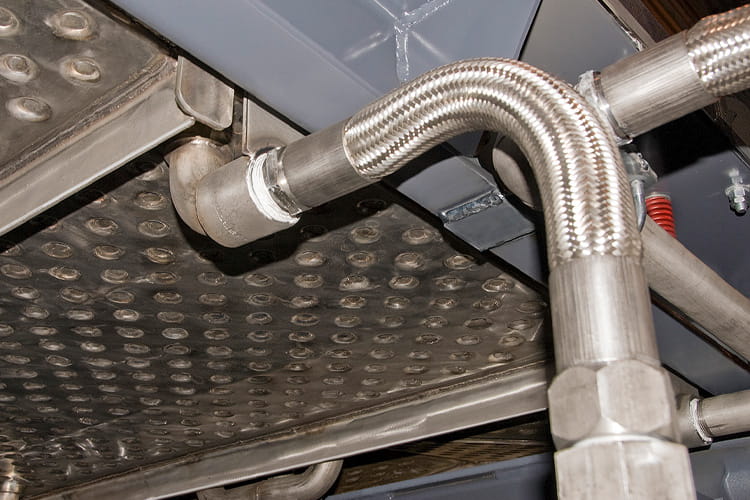
Jacketed designs provide indirect heating and cooling while conveying products.
Manual or automatic bypass gates provide directional routing of product. Separate, independent troughs can also be integrated into Carrier conveyors.
Screening decks can be added for screening and sizing product.
Polished trough and special coatings assist in conveying sticky products.
Anwendungen
Conveys abrasive bauxite and clay with controlled vibratory motion for consistent material flow. Rugged construction handles dense, variable feed while minimizing buildup and supporting continuous downstream processing. Acts as a self-contained processing unit for minerals like bauxite and clay by combining conveying with heavy-duty operations like screening, drying, and cooling.
Transfers cementitious materials and SCMs at controlled feed rates using engineered vibratory motion. Enclosed configurations can minimize dust while maintaining consistent material distribution to downstream equipment. Carrier’s vibrating conveyors have fewer moving parts than belt or screw conveyors, reducing maintenance and preventing thermal shock.
Carrier’s vibrating conveyors move powders, crystals, granules, and specialty compounds through chemical plants while providing multi-functional processing. They prevent product degradation and contamination by keeping materials in a continuous, gentle motion along an enclosed, smooth trough. Adjustable vibratory parameters accommodate varying bulk densities and flow characteristics while supporting precise material delivery.
Transports coal with controlled vibration that maintains consistent bed depth and feed rate. Heavy-duty construction accommodates abrasive material while enclosed designs can help contain dust and fugitive emissions. Conveyors can be configured to simultaneously perform tasks like drying, cooling, screening, and dewatering.
Conveys crushed coal and mineral products under demanding, abrasive conditions. Engineered vibration maintains reliable material movement while robust trough construction withstands high-density and irregular feed materials. Our vibratory conveyors can perform simultaneous processes – such as scalping, screening, drying, and cooling – in a single unit.
Gently conveys fertilizer granules while maintaining consistent feed rates and minimizing particle degradation. Controlled vibration reduces product buildup and provides uniform distribution to screening, cooling, storage, or packaging systems.
Provides gentle, sanitary conveying of powders, granules, and finished products. Controlled vibration maintains consistent product flow while sanitary construction supports efficient cleaning and contamination control.
Built to withstand extreme temperatures and harsh conditions, foundry operations optimize their lines by integrating multiple processes such as separating sand, cooling, and sorting into a single, continuous system.
Transports abrasive glass cullet and processed glass with controlled vibratory motion. Durable trough construction maintains consistent flow while accommodating sharp, irregular particles and demanding recycling environments.
Conveys dense, abrasive limestone at controlled rates between crushing, screening, and processing operations. Engineered vibratory motion maintains uniform material flow while minimizing plugging and accumulation. Because limestone is highly abrasive, Carrier’s conveyors are built with specialized heavy-duty troughs, including abrasion-resistant (AR) steel and ceramic linings.
Provides controlled transfer with gentle handling of lithium-bearing and critical-mineral materials between processing stages. Enclosed conveying can limit dust and contamination while maintaining consistent feed rates for downstream equipment. Custom-engineered to transport, dry, cool, and screen high-value lithium and other critical battery minerals.
Convey pellitized products such as biomass, plastics, and animal feed without the friction, breakage, or tumbling often caused by traditional belt or screw conveyors. Gently conveys pellets with controlled vibratory motion to minimize degradation and fines generation. Uniform material distribution supports consistent feeding to cooling, screening, storage, or packaging equipment.
Gently move, dry, cool, and separate fragile bulk pharmaceutical powders and granules. Operating on an energy-efficient natural-frequency design, our conveyors deliver controlled, gentle conveying in sanitary configurations. Consistent vibratory motion supports accurate material transfer while minimizing product degradation and contamination risks.
Conveys pellets, resins, and synthetic materials with gentle vibratory motion and controlled feed rates. Consistent material movement minimizes pellet damage while supporting reliable downstream processing.
Targeted vibration and custom non-stick troughs prevent sticky rubber from bed matting, bridging, and clumping. Cool down hot rubber, dry moisture from crumb rubber, scalp out irregular sizes, and dewater wet material with consistent feed rates for screening, recycling, and downstream processing.
Conveys abrasive and corrosive salt products with controlled vibratory motion and application-specific trough construction. Uniform material movement supports reliable feeding while minimizing buildup and uncontrolled product flow.
Handles abrasive sand and silica sand with controlled, continuous vibratory conveying. Rugged trough construction and uniform material movement provide reliable transfer between drying, cooling, screening, and storage operations.
Conveys lightweight, irregular shredded used beverage cans using controlled vibration for consistent material distribution. Uniform feeding improves performance of downstream separation, sorting, and metal recovery equipment.
Moves cohesive wet cake using engineered vibratory forces that promote positive material movement. Controlled vibration reduces sticking and buildup while providing consistent transfer to drying or downstream processing equipment.
Conveys wood chips, fibers, bark, and biomass using controlled vibration for uniform material distribution. Engineered trough designs accommodate lightweight, irregular particles while maintaining reliable continuous flow.
Galerie
Vibrating Conveyors FAQs
Vibrating conveyors are used to move bulk materials efficiently through industrial processing lines. They provide controlled, continuous material flow for applications involving hot, abrasive, fragile, or irregular materials.
Carrier vibrating conveyors are engineered for aggregates, foundry sand, biomass, minerals, chemicals, food products, recycled materials, wood products, and other bulk solids with varying particle sizes and temperatures.
Unlike belts or chain conveyors, vibrating conveyors have fewer moving parts and no tracking issues. This reduces wear, minimizes downtime, and lowers long-term maintenance costs.
Yes. Carrier vibrating conveyors are commonly designed for hot material applications such as clinker, foundry shakeout, kiln discharge, and thermal processing systems.
Natural-frequency designs improve energy efficiency, reduce stress on components, and extend equipment life while maintaining stable material flow.